What Is a Downdraft Table? How It Works, Types & Uses

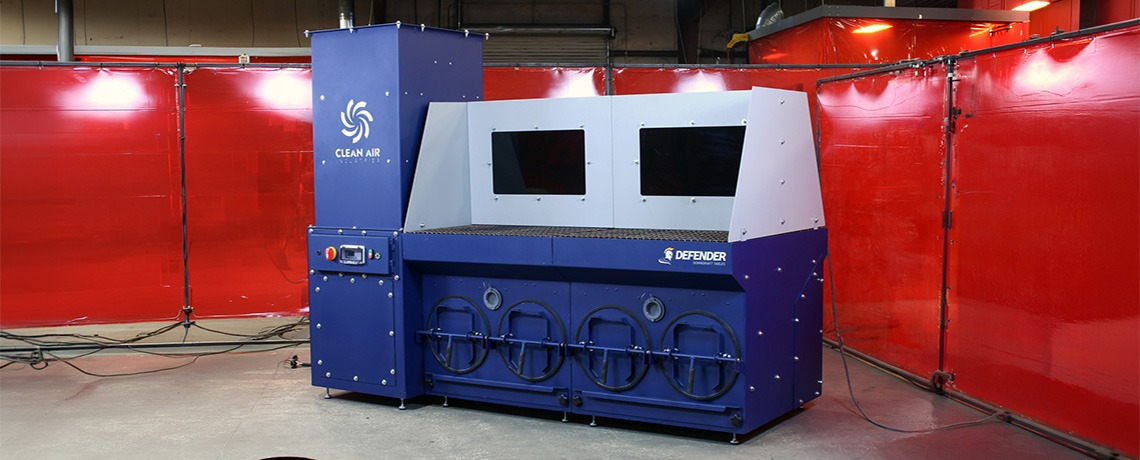
A downdraft table is a ventilated workstation that captures dust and fume at the source. A fan draws air down through a perforated work surface and into filters, removing contaminants from grinding, welding, sanding, and finishing before they spread through the shop.
Because capture happens where contaminants are generated, downdraft tables are one of the most direct ways to control exposure during grinding, welding, deburring, and finishing. This guide explains how they work, the specs that matter, the main types, and when another solution is a better fit.
How a downdraft table works
A fan inside or connected to the table creates negative pressure below the work surface, so air and contaminants are pulled down instead of rising toward the operator.
- Air is drawn down through the perforated surface. Dust, sparks, and fume generated on the table are pulled into the openings as they form.
- Sparks and heavier particles are knocked out. Spark arrest components stop sparks before they reach the filters, and heavier grinding particles drop out of the airstream.
- Filters capture fine particulate. Defender downdraft tables use flame-retardant 80/20 cellulose/polyester cartridge filters rated MERV 11 as standard, with nanofiber filter and HEPA afterfilter upgrades available.
- Filters are cleaned or replaced. Some tables, including Defender industrial models, have a built-in cleaning system that dislodges collected dust from the filters into a removable dust drawer. Others use disposable filters that are replaced once they load with dust. On ducted tables, filter cleaning happens at the central dust collector.
- Clean air is returned or exhausted. Self-contained tables recirculate filtered air into the shop. Ducted tables send air to a central dust collector for filtration.
Key downdraft table specs explained
Four specs determine how well a downdraft table performs: airflow, face velocity, filtration, and noise.
Airflow (CFM) is the volume of air the table moves per minute. More CFM allows a larger work surface, but on its own it doesn’t tell you how strongly the table captures.
Face velocity (FPM) is the speed of air at the work surface, and it’s what actually pulls contaminants down. It’s calculated as:
FPM = CFM ÷ work surface area (sq ft)
Manufacturers don’t all use the same area. True face velocity divides by the entire work surface. Some spec sheets divide by the perforated open area only, which produces a higher number. When comparing tables, check which area each figure uses.
Filtration is rated by MERV (Minimum Efficiency Reporting Value) or HEPA. Higher ratings capture finer particles. Fine weld fume and hazardous metals may call for a HEPA afterfilter.
Noise is measured in dBA at a set distance. It rises with motor size, so confirm the level at the operator’s position.
Defender industrial downdraft table specs:
| Model | Work surface | Area (sq ft) | Airflow (CFM) | True face velocity (FPM) | Motor | Noise @ 5 ft |
|---|---|---|---|---|---|---|
| DDT-4×3 | 4 × 3 ft | 12 | 4,200 | 350 | 5 HP | 73 dBA |
| DDT-4×6 | 4 × 6 ft | 24 | 6,480 | 270 | 10 HP | 77 dBA |
| DDT-4×9 | 4 × 9 ft | 36 | 9,000 | 250 | 15 HP | 81 dBA |
The 4×9 moves the most air but has the lowest face velocity, because its airflow is spread over the largest surface. Compare all downdraft table models.
Types of downdraft tables
Downdraft tables differ mainly in where the air goes after capture and how much surface they cover.
Portable self-contained tables combine the fan and filters in a compact unit that can be moved between workstations. The Defender 2×3 Portable Downdraft Table delivers 1,200 CFM for spot grinding and light welding.
Industrial self-contained tables are larger, fixed workstations with their own fan and filters. Defender Industrial Downdraft Tables come in 4×3, 4×6, and 4×9 configurations from 4,200 to 9,000 CFM, with built-in filter cleaning.
Ducted (remote) tables connect to a central dust collector, which provides the airflow and filtration. This makes them cost-effective when a facility needs several tables. See Defender Ducted Downdraft Tables.
Tables with walls or hoods add back walls, side walls, dividers, or an overhead hood to contain fume that rises above the surface. Defender options include metal or clear Lexan walls and 3, 6, or 9 ft hoods.
Common downdraft table applications
Downdraft tables work best for tasks done on a bench, where contaminants are generated at or just above the work surface.
- Metal grinding: captures grinding dust and sparks thrown off the wheel.
- Welding: captures weld fume on small and medium parts. Excessive downdraft can pull shielding gas away from MIG and TIG welds and cause porosity, so airflow should match the process.
- Brazing and soldering: captures flux smoke and fume at the joint.
- Deburring and polishing: captures fine metal dust and compound residue.
- Sanding and finishing: captures fine dust before it settles on parts and equipment.
Welding and training programs also use downdraft tables as dedicated student workstations. See vocational solutions.
Downdraft table vs. other fume and dust control options
A downdraft table is the right choice when work happens on a bench. For larger parts, mobile work, or whole-shop air, another system usually fits better.
| Solution | How it captures | Best for | Main limitation |
|---|---|---|---|
| Downdraft table | Pulls air down through the work surface | Bench grinding, welding, and finishing on small to medium parts | Parts must fit on the table; rising fume can escape without walls or a hood |
| Fume capture arm | Hood positioned at the arc or source | Fixed welding stations and larger parts | Hood must be repositioned as the work moves |
| Portable fume extractor | Mobile unit with an arm or hood | Maintenance, job shops, and changing layouts | Covers one workstation at a time |
| Welding and grinding booth | Enclosed workspace with built-in extraction | High-volume work and containing sparks and noise | Larger footprint and higher cost |
| Ambient air cleaner | Filters general shop air | Residual fume that source capture misses | Doesn’t protect the operator’s breathing zone on its own |
Many facilities combine source capture, such as a downdraft table, with ambient filtration for the remaining airborne particulate. Read more on why source capture beats general ventilation.
When a downdraft table isn’t the right fit
A downdraft table only captures what happens close to its surface. Consider another solution, or add walls or a hood, when:
- Parts are larger than the table or cover most of the perforations, which blocks airflow and leaves dead zones.
- Fume rises well above the surface, as with tall assemblies or high-heat processes, and escapes the capture zone.
- The dust is combustible or reactive. Aluminum, magnesium, titanium, and similar dusts need a system designed for that hazard, often identified through a Dust Hazard Analysis. See NFPA 660 for current requirements.
- Work moves around a large part or area, where a fume arm, portable extractor, or booth covers the space better.
Downdraft table maintenance
Capture drops as filters load, so routine maintenance directly affects performance.
- Empty the dust drawer or collection tray before it fills.
- On self-cleaning tables, run the cleaning cycle and replace filters when cleaning no longer restores airflow. On tables with disposable filters, replace them on the manufacturer’s schedule or when airflow drops.
- Keep the perforated surface clear of buildup and debris.
- Inspect the fan, motor, and door seals on the schedule in the manufacturer’s manual.
Defender owners can find the full schedule in the Defender user manual.
Frequently asked questions
Do downdraft tables work for welding?
Yes, for welding small and medium parts on a bench. Airflow should match the process, because too much downdraft can pull shielding gas away from MIG and TIG welds. Walls or a hood help contain fume that rises above the surface.
How much CFM does a downdraft table need?
It depends on the table’s surface area and the face velocity the process requires: CFM = target FPM × surface area in sq ft. For example, a 4×6 table (24 sq ft) at 270 FPM requires 6,480 CFM.
What is a good face velocity for a downdraft table?
It depends on the process. Defender industrial tables deliver 250 to 350 FPM true face velocity, calculated across the full work surface.
Are downdraft tables safe for aluminum dust?
Only if the system is designed for it. Aluminum and other combustible metal dusts often require a wet table or a ducted table connected to a suitable collector, based on a Dust Hazard Analysis.
Downdraft table or fume extractor: which is better?
A downdraft table is better for bench work on parts that fit on the table. A fume arm or portable fume extractor is better for larger parts, fixed welding stations, or work that moves.
Can a downdraft table help with OSHA compliance?
Yes, by reducing worker exposure to dust and fume at the source. OSHA doesn’t certify equipment, so compliance depends on measured exposure levels, proper use, and maintenance. See OSHA’s fact sheet on controlling welding fume and gases.
Find the right downdraft table
Defender downdraft tables are built in the USA by AWS-certified welders, in portable, industrial, and ducted configurations from 1,200 to 9,000 CFM.
- Compare Defender downdraft table models
- Read the guide to choosing the right downdraft table
- Request a quote from a Clean Air application specialist
- Category: Downdraft Tables, Grinding, Laser Cutting, Welding